
 Tiếng Việt
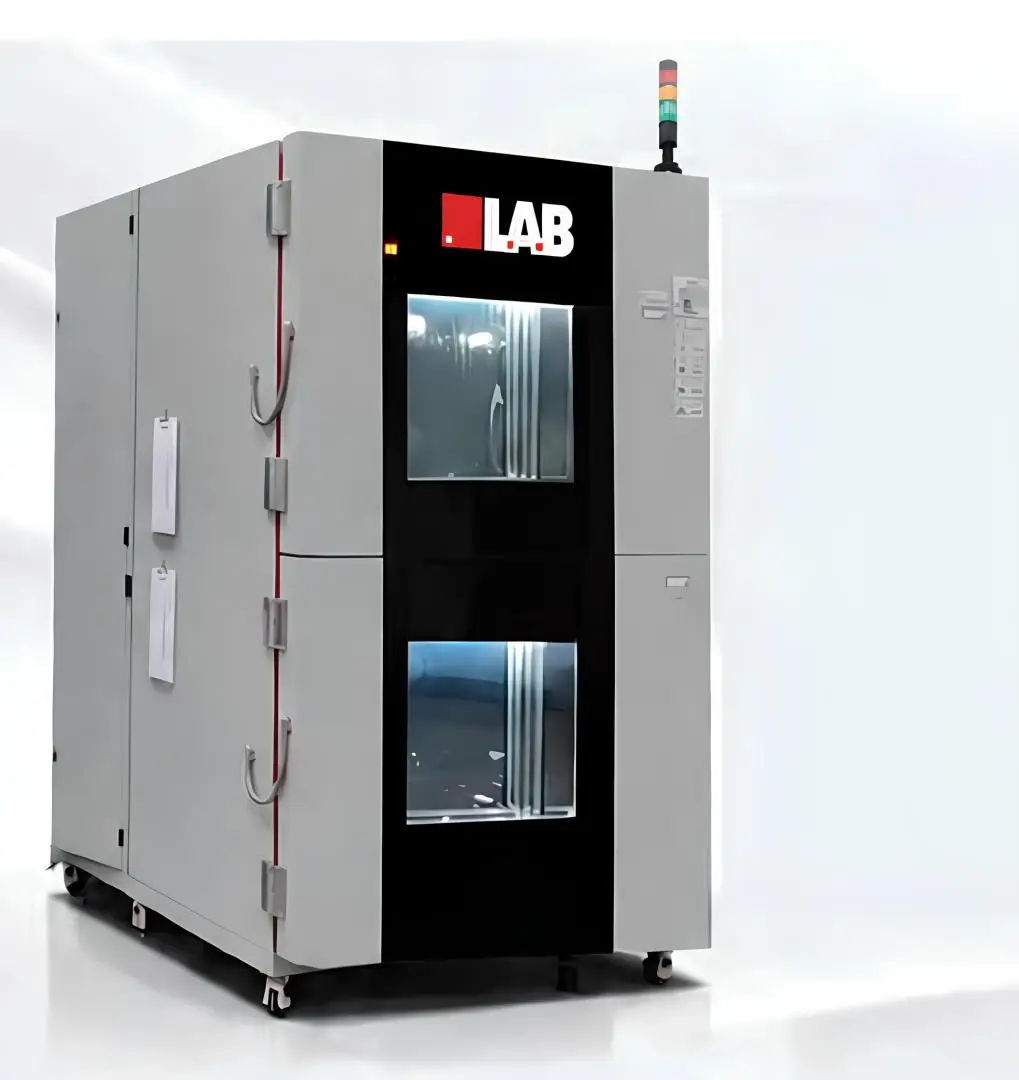
TC-M-1000DH Temperature & Humidity Test Chamber
Get the genuine TC-M-1000DH Temperature & Humidity Test Chamber from Lab Equipment (Made in USA), distributed by Maxlab. The exclusive MultiCell™ architecture increases lab throughput by 3x and cuts energy consumption up to 50%. Explore full technical specifications now!
Product Information
Technological Breakthrough with TC-M-1000DH Temperature & Humidity Test Chamber from L.A.B USA
In the modern industrial manufacturing era, ensuring product quality and reliability before launching to the market is a vital factor for any business. To meet the stringent standards of industries such as battery manufacturing, electronics, automotive, pharmaceuticals, and medical devices, testing laboratories require an environmental testing solution that is both highly precise and cost-effective.
Understanding this demand, Maxlab is proud to introduce a groundbreaking solution: the TC-M-1000DH Temperature & Humidity Test Chamber – a technological masterpiece from the prestigious brand L.A.B (USA). Equipped with the exclusive TrueClimate™ MultiCell environmental chamber architecture, this equipment redefines the concepts of efficiency and energy savings in the reliability testing industry.
1. Introduction to L.A.B Testing Equipment – Peak Technology from the USA
When it comes to packaging validation solutions and product reliability testing, Lab Equipment from L.A.B is always a trusted name guaranteeing the highest premium quality. With a long-standing history of over 90 years of operation since 1933, L.A.B has built a solid empire thanks to its deep expertise in testing engineering and an extensive global service and support network.
All products from the brand, including the TrueClimate™ chamber series, come with clear certifications of origin: Made in USA (researched, designed, and manufactured directly at the company’s facility in Itasca, Illinois, USA). The strict American manufacturing processes ensure that the equipment possesses outstanding mechanical durability and the capability to run continuously 24/7 for many years without failure. This delivers an extremely high return on investment (ROI) for businesses in Vietnam when investing through the official distributor, Maxlab.
2. The Ultimate Differentiator: Exclusive MultiCell™ Architecture
The biggest weakness of traditional environmental test chambers (Conventional Architecture) on the market is their single-tasking nature. One chamber consists of only one test space and one complete climate system. When a business needs to increase testing capacity or run multiple different temperature-humidity profiles simultaneously, they are forced to purchase additional machines. This leads to negative consequences: occupying more factory floor space, consuming double the energy, and driving up initial capital expenditures.
To thoroughly solve this economic puzzle, the TC-M-1000DH Temperature & Humidity Test Chamber utilizes the revolutionary L.A.B Exclusive MultiCell™ Architecture. This technology works on the principle of decoupling the core environmental conditioning system from the test cells:
- One Integrated Climate Core™: Acts as the central power hub, centralizing all cooling, heating, humidity generation, air circulation, and energy management functions into a single platform.
- Multiple Independent Testing Cells: The TC-M-1000DH model is configured as a Dual-Cell system (2 independent testing chambers arranged in a horizontal Left & Right layout).
- Dynamic Resource Distribution: The centralized Integrated Climate Core™ automatically and dynamically allocates climate resources and energy sessional power to each testing cell based on the actual demand of the active profile program.
Thanks to this revolutionary architecture, the two test cells of the TC-M-1000DH model can maintain completely independent temperature and humidity profiles, programs, and data tracking without any cross-interference.
3. Impressive Technical Specifications of the TC-M-1000DH Temperature & Humidity Test Chamber
The TC-M-1000DH model features industry-standard technical specifications designed to handle large-sized specimens or a high volume of samples within a single testing cycle:
- Test Space Volume of Each Cell: Up to 1000 Liters per cell, providing an exceptionally spacious testing zone (equivalent to 35.3 ft³ on each side).
- Internal Dimensions of Each Cell (W*D*H): 1000mm * 1000mm * 1000mm. The perfect cubic shape allows technicians to easily arrange sample trays.
- External Overall Dimensions (W*D*H): 2590mm * 2165mm * 2180mm.
- Ultra-Wide Temperature Range: Ability to control temperatures from -38°C to +180°C (equivalent to -36.4°F to +356°F).
- Temperature Fluctuation: Extremely tight control at ≤ ± 0.5°C, ensuring the climate inside the chamber remains perfectly stable.
- Temperature Uniformity: ≤ 2°C at temperatures up to +150°C, ensuring that every single point within the test space shares the exact same thermal environment.
- Temperature Change Rate (Heating / Cooling): Reaches 3°C/min, significantly shortening waiting times when performing thermal cycling tests.
- Comprehensive Humidity Range: Controls humidity from 10%RH to 98%RH (within the temperature range of +10°C to +90°C).
- Removable Partition Between Cells: This is a highly valuable, exclusive optional feature for the TC-M-1000DH model. When testing extra-large or over-length specimens, operators can easily remove the center partition wall to transform two independent cells into a single, massive testing zone. When needed, the partition can be re-installed just as easily to restore the two fully independent climate zones.
4. 5 Core Advantages for Optimizing Business Operational Costs
Distributed officially by Maxlab, the TC-M-1000DH Temperature & Humidity Test Chamber delivers five core competitive advantages for R&D centers and manufacturing plants:
4.1. Lower Total Investment
Instead of allocating a budget to purchase two standalone test chambers, you now only need to invest in a single TC-M-1000DH system. Having one integrated climate core serve multiple independent cells drastically cuts hardware component costs, offering clear economic performance and a much stronger ROI.
4.2. Ultra-Low Energy Consumption
The smart energy management system takes full advantage of surplus energy. When one chamber is running a profile that releases heat, that excess energy can be automatically redirected to power independent tests in the neighboring chamber. Independent tests prove that the TC-M-1000DH achieves up to 50% total energy savings compared to running two standalone units of identical specifications.
4.3. Maximized Space Savings
Factory floor space is always a premium asset. With its integrated dual-chamber layout arranged horizontally on a single machine base, the TC-M-1000DH reduces physical space occupied (footprint) by 30% to 50% compared to placing two separate machines. Your lab room becomes significantly cleaner, more professional, and highly optimized.
4.4. Higher Testing Throughput
Businesses can conduct two separate validation tests with completely different temperature-humidity profiles simultaneously (for example, one cell running a high-temperature aging test at +85°C/85%RH, while the other runs a low-temperature cycle at -30°C). This ensures 2x to 3x testing capacity productivity for your lab, cuts idle scheduling time by 50%, and accelerates product time-to-market.
4.5. Future-Ready Flexibility
The expandable capability via the removable center wall allows the chamber to effortlessly adapt to evolving project requirements in the future. You will never have to worry about your equipment becoming obsolete or failing to accommodate growing component dimensions as your manufacturing lines upgrade.
5. Smart Management System and In-House-Developed Controller
In addition to heavy-duty hardware built to strict US standards, the TC-M-1000DH chamber is integrated with an intelligent management software system, making operations both user-friendly and absolutely safe:
- In-House-Developed Control System: Optimized closed-loop regulation algorithms deliver high-precision, rock-solid temperature and humidity control.
- Graphical Intuitive User Interface: A vivid touch screen offers a visual user experience, allowing operators to easily create and execute complex test profiles without any programming expertise.
- Real-Time Energy Monitoring: Live tracking of device power consumption with custom time-period energy statistics for full power usage traceability and easy factory energy audits.
- Traceable Data Backup: An onboard database securely stores up to 12 months of full operational history locally, making it easy to download and trace charts or logs whenever an anomaly occurs.
- Fault Monitoring & Early Warning: The system constantly monitors critical operational parameters, displays the exact fault location if an error occurs, and activates safety protection to safeguard both your samples and the equipment.
6. Maxlab – Your Trusted Partner for Reliable Testing Solutions
When choosing high-tech laboratory and testing equipment, selecting a reputable distributor with proven technical capabilities is paramount. Maxlab is proud to be the official provider of the TC-M-1000DH Temperature & Humidity Test Chamber from L.A.B USA in the Vietnamese market.
By partnering with Maxlab, customers receive:
- 100% genuine imported equipment with full certifications of origin and quality papers (CO/CQ).
- In-depth technical consultation to customize equipment configurations tailored precisely to the testing standards of your specific industry (Batteries, electronics, pharmaceuticals, automotive, etc.).
- A team of highly experienced, factory-trained engineers handling turnkey installation, calibration, operator training, and routine maintenance.
- Long-term official warranty policies with readily available replacement components, promising to resolve technical issues in the shortest time possible to prevent any disruption to your production chain.
Let Maxlab accompany your business in elevating product quality. Contact us today to receive detailed quotes and the best promotional programs for this premium environmental test chamber system!